Hey everyone, it’s Jake here—head of operations at your go-to reaming machine supplier, and if you’ve ever been part of a manufacturing shop floor, you know installing a new machine isn’t just plugging it in and hitting “go.” I’ve seen folks skip the environment prep, then spend weeks troubleshooting weird alignment issues or weird wear on tooling parts, and it’s always avoidable. Today I’m breaking down exactly what you need for a solid reaming machine install—no overly jargon-heavy stuff, just real, shop-tested details I’ve picked up over 12 years of working with guys who use these machines every single day. Reaming Machine
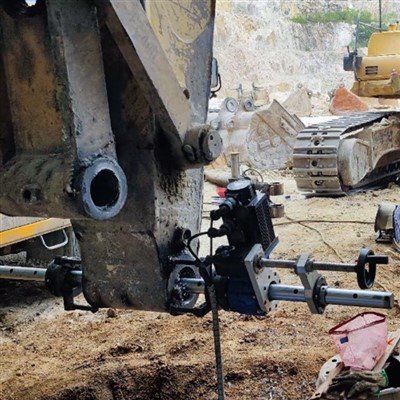
First off, let’s get one thing straight: reaming machines aren’t your grandma’s drill press. They’re precision tools designed to turn a rough hole (think from a drill or boring bar) into a tight, smooth, accurate one—usually within thousandths of an inch. If your environment’s off, you won’t hit those specs, no matter how fancy the machine is. Let’s start with the big one people sleep on: floor requirements. I’ve heard so many horror stories of install crews showing up, only to find the shop floor’s got a 1/4-inch sag in the 10-foot area where the machine’s going. That’s a non-starter, full stop.
What’s the actual number we go over with every customer? For most of our standard production reamers, you need a reinforced concrete floor with a minimum compressive strength of 3,000 PSI. Wait, 3,000? That’s not overkill—remember, a reaming machine’s exerting consistent, controlled pressure, usually 5 to 20 tons depending on the model. If your floor’s too soft, it’ll settle just enough during a deep cut to throw off the hole’s diameter and roundness. And it’s not just strength—levelness is make-or-break. We recommend checking level in two axes (X and Y, across the machine’s base) with a precision level that can read to 0.002 inches per foot. A lot of guys use a basic 0.01 inch level and call it good, but that’s like using a ruler to measure a credit card chip—won’t cut it. Also, leave enough clearance around the machine for maintenance: at least 3 feet on all sides, plus 5 to 6 feet behind the control panel so someone can actually get in there to fix a wiring harness or change the coolant pump without squeezing through a gap no bigger than a shoebox. I once had a customer who tried cramming a machine into a 2-foot gap, and they ended up taking a sledgehammer to a cinder block wall a week later—total waste of time and money.
Next up: power supply. This is another area where cutting corners causes headaches. Reaming machines run on three-phase power, full stop. Single-phase might work for tiny home garage tools, but our production-grade reamers need the steady, balanced voltage three-phase provides to avoid motor stutters and inconsistent speed. What voltage? Most of our US customers use 480V, 60Hz, but we work with global clients too—just let us know, and we can adjust the motor specs ahead of time. The big rule here: no daisy-chaining the machine to other heavy equipment. If your shop’s already running a CNC lathe, a welding robot, and a parts washer off the same circuit, that’s a recipe for voltage drops when everything kicks on. We always suggest a dedicated circuit, size-wise: calculate the machine’s full-load amperage (FLA) and add 20% as a buffer. For example, our mid-sized reamer has an FLA of 40A, so you need a 50A circuit. And don’t skip the grounding—we see so many machines with weird electrical noise because the ground is weak, which messes up the sensor that controls reamer feed rate. That noise will make the cut uneven, leaving little ridges in the hole wall you can feel with your finger.
Coolant and air supply—wait, most new guys forget reaming uses coolant, right? Yeah, you’re not dry-cutting steel here. Reaming generates a ton of heat, and that heat will warp the tool and the workpiece before you finish the first part if you don’t have the right coolant setup. First, the coolant system: it needs to handle both the volume and the temperature. Our machines require a coolant flow rate of at least 15 gallons per minute, at 10 to 30 PSI, directed right at the cutting edge of the reamer. If your flow is too low, you’ll get built-up edge on the tool, which makes holes too big. Also, coolant temperature should stay between 60°F and 80°F. If it’s hotter than that, it expands and throws off the hole’s size—we’ve had a customer in Texas deal with a 0.005-inch size variation because their coolant tank sat in direct sunlight all day. We ended up adding a chiller unit, and it fixed the problem overnight.
Then there’s compressed air. Most reamers use air for two things: coolant filtration (to keep the lines from clogging) and some models use air to eject the part after a cut. You need a dry, oil-free air supply at 90 to 110 PSI. If there’s moisture in the air line, it’ll mix with coolant and cause corrosion in the machine’s internal valves, leading to leaks that slow down operation. We always tell customers to install a water separator and air dryer right at the machine inlet—don’t try to use the existing shop air filter from across the shop; it’s not enough.
Environmental conditions beyond the machine itself—shop climate, vibration, dust. Let’s talk about dust first: metalworking shops are dusty, duh, but fine metal shavings can get into the machine’s control box, sensors, and linear guides, causing wear over time. We recommend keeping dust levels under 10 milligrams per cubic meter (that’s OSHA’s limit for metal dust, by the way) using a local dust collector right next to the reamer. No need for a huge central system, just a hood that captures shavings as they come off the cut.
Temperature and humidity in the shop: keep it between 60°F and 90°F, humidity between 30% and 70%. Extreme heat causes the machine’s metal parts to expand, extreme cold makes lubricants thick and hard to circulate. Humidity over 70% leads to rust on the tooling and machine base, which is a slow killer—you won’t notice it for months, but it’ll make alignment drift over time. And vibration—this is a big one if your shop has other heavy machinery like forges or stamping presses that run 24/7. If the reamer is within 10 feet of a stamping press, the constant vibration will throw off the machine’s alignment. We suggest checking vibration levels with a vibration meter—keep it under 0.5g peak acceleration at the machine’s base. If your shop has that kind of vibration, you’ll need to add vibration isolators under the reamer’s base; they’re not that expensive, and they save you from years of bad holes.
Wait, let’s add a quick real-world example to make this concrete. Last year, we worked with a customer in Detroit who skipped checking the floor level. They installed a 20-inch reamer in a shop with a slightly sagged floor, and within a week, their production rate dropped by 30%. The holes were coming out round within spec, but the straightness was off, so parts wouldn’t fit into the assembly. Their install crew just assumed the floor was level because it looked good—we did a precision level check and found it was off by 0.015 inches across the base, enough to shift the reamer head’s alignment. They ended up pouring a 2-inch concrete pad specifically for the machine, and production was back to normal in 10 days. That’s the kind of avoidable mistake we’re talking about.
Another thing most people overlook: access for future upgrades and maintenance. Our reaming machines are modular—you can add automatic tool changers, coolant thru systems, or robotic part loaders down the line. If you pack the machine too tight against walls or other equipment, you can’t bolt on those upgrades without rearranging half the shop. We always suggest leaving 4 feet of clearance on the side where the control panel and any future upgrade ports are, so a technician can plug in new wiring or parts without tearing out shelving.
Now, let’s wrap this up with what this all means for you guys—whether you’re a job shop with 5 machines or a big automotive plant. Getting the install environment right doesn’t just mean avoiding headaches later; it means better part quality, less downtime, longer machine life, and lower operating costs. I’ve seen machines last 15+ years when installed correctly, and ones that die in 5 because of a bad floor or bad power.
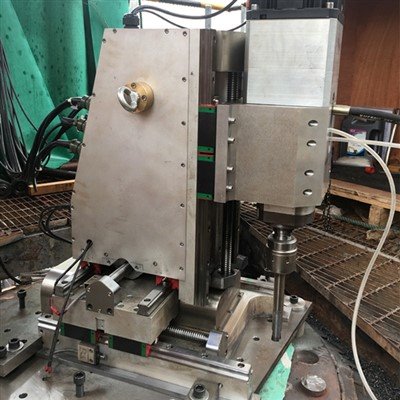
If you’re planning on picking up a reaming machine (or upgrading your current setup), don’t wing the install. Send us your shop floor specs, power details, whatever you have, and we can walk you through exactly what you need to prep. No sales pitches, no vague advice—just real, actionable stuff from someone who’s installed these machines hundreds of times. If you have questions about a specific model or your shop’s setup, hit us up to chat. We’re here to make sure your reaming machine works as hard as you do, without the stupid avoidable problems.
Portable Milling References:
- Machinery Installation Requirements: Concrete Floor Specifications, American Machinist, 2022
- Precision Metalworking Machine Environmental Standards, National Institute of Metalworking Skills (NIMS), 2021
- Power and Utility Requirements for CNC Machining Equipment, Manufacturing Engineering Association, 2020
- Coolant and Compressed Air Best Practices for Reaming Operations, Society of Manufacturing Engineers (SME), 2023
- Vibration Isolation for Industrial Machine Tools, International Organization for Standardization (ISO) 10816-3, 2019
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional reaming machine manufacturers and suppliers in China. We warmly welcome you to buy cheap reaming machine for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
